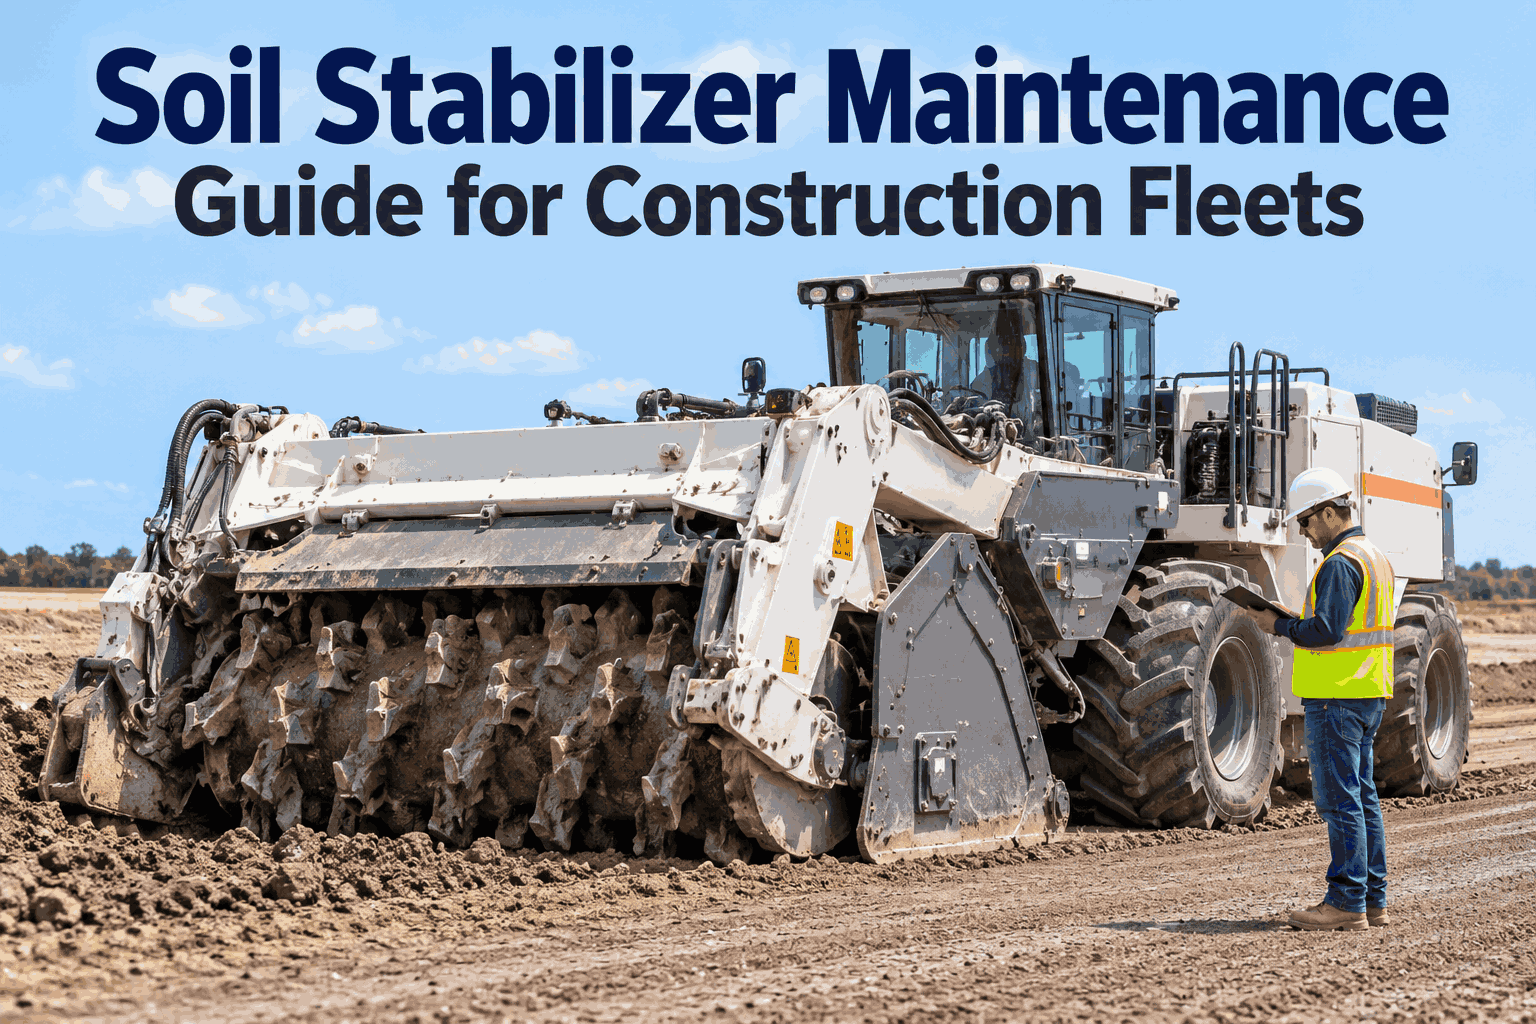
Soil stabilizer maintenance is really the upkeep of one process: raw soil in, rotor cuts and mixes while binder sprays, stabilized base out. Every stage wears — the cutting bits most of all — and the machine earns only while that rotor turns, running on hours, not miles. Keep the process healthy and the mix stays on spec. Book a demo to see it scheduled by hours.
Maintain the Process, Not Just the Machine
A stabilizer is a soil-in, base-out production line on wheels. The health of every stage decides your mix quality and your running cost — so that's what a real program keeps in check.
The two hot stages — the rotor and the binder spray — are where quality is won or lost, so the program starts there and works out to the rest of the machine.
The rotor: everything radiates from herethe wear points around the cutting drum
Look after the rotor and most of the stabilizer looks after itself. It is the drum that does the cutting and mixing, and its bits are the fastest-wearing part on the machine. These are the points that ring the rotor and need eyes on them, each one feeding back into how well the drum cuts.
The bits and toolholders are inspected together, because a worn holder ruins a fresh bit and a snapped bit hides a cracked holder. The rotor hood and its liners take the abrasive blast of thrown material, so worn liners and a poor door seal let material escape and change the mix.
The rotor bearings, though slow to fail, give the earliest warning of trouble through a new growl or a trace of play — catch that and you avoid a full drum rebuild. None of these are hard checks, but they're easy to skip when a machine is mid-job, which is exactly why they belong on a schedule rather than a memory.
A bit that's dull, a holder that's cracked, a worn hood liner — each quietly drags the whole cut down. Book a demo to see the rotor checks recorded with a photo each pass
Walk the rest of the machinefront to back, the systems that keep the rotor fed and moving
Beyond the drum, the stabilizer is a chain of systems that either feed the rotor, meter the binder, or move the machine. Walk it end to end and each has a couple of tells worth catching before they reach the mix or the shop. Because these systems run on their own OEM hour intervals, the walk is as much about logging where each one sits against its next service as it is about spotting damage.
Spray & binder system
Nozzles clear, spray bars clean, pump and flow rate on target. A partly clogged bar means uneven binder and off-spec mix — flow-test it rather than assume.
Drive, clutch & belts
Belt tension and wear, clutch engagement, driveline noise. Slip here shows up straight away as lost cutting power at the rotor.
Hydraulics & depth control
Pumps, cylinders, hoses and fluid for leaks and pressure. Hydraulics run the rotor hood, cut depth and steering on most machines.
Engine, cooling & undercarriage
Filters and cooling clog fast in dusty cutting work; tracks or tyres and final drives carry the load. Service both on OEM hours.
Grouping the walk this way means nothing gets skipped when the site is running hot. Start free and put the whole machine walk on one template
Dull bits cost you before they breakthe price of running past the wear curve
The reason bit maintenance matters isn't a sudden failure — it's the slow tax you pay running worn bits. As they dull, fuel burn and rework climb together while cut quality falls, so the machine costs more with every pass long before anyone calls it broken. This is what running to failure really looks like.
The trap is that a worn stabilizer still works — it still turns soil, just slower, thirstier and less uniformly — so nobody flags it. The cost hides in the fuel log and the occasional re-do, not in a breakdown report. Tracking bit hours against inspection findings is what turns that invisible drift into a scheduled, planned change while the numbers still look fine.
Change on the curve, in the yard, and you never reach that last bar. Start free and track bit hours so the change is planned, not forced
Reactive vs scheduled, side by sidewhy the one machine nobody schedules leaks the most money
A stabilizer is often the odd machine out in a mixed fleet — the one whose maintenance rides on memory until the mix comes out wrong. On a machine whose wear part controls both quality and fuel, that reactive habit is the most expensive one you can keep.
Reactive
Checked when the mix goes wrong — the worst time to find out.
Bits run past their curve, quietly burning fuel every pass.
Rotor and spray faults surface mid-job, on site.
No record to prove the machine was maintained.
Scheduled with HVI
Bit wear and spray flow-test on a recurring hours schedule.
Automatic prompt before every service is due.
Faults caught in the yard on a planned check.
Photo-verified history, searchable for any audit.
The machine moves from reactive to scheduled without adding a single head to the shop. Book a demo to see the stabilizer program off memory and on a schedule It slots into the same hours-based approach as any OEM maintenance schedule.
From a grading contractor's maintenance manager
The stabilizer was the one machine nobody owned on the PM side — it got looked at when the mix came out wrong, the worst time to find out. We were burning bits and fuel and blaming the operator. Once we put rotor bit hours and a spray flow-test on a schedule with a photo each time, the mix got consistent and the fuel came back down. The machine wasn't the problem; not scheduling it was.
Soil stabilizer maintenance: quick answers
What does soil stabilizer maintenance cover?
It follows the machine's process: the rotor and cutting bits, the water or binder spray system, the drive, clutch and belts, the hydraulics and depth control, and the engine, cooling and undercarriage. The rotor and spray get the closest attention because they directly control mix quality and running cost.
How often should rotor cutting bits be replaced?
Bits are a consumable that wear on a curve, so they're changed on hours and inspection findings, not a fixed date. The aim is to change at the "worn" stage — where fuel and mix quality start slipping — instead of the "spent" stage that forces unplanned downtime. Exact life depends on soil abrasiveness and the OEM.
Why schedule stabilizer maintenance by hours instead of the calendar?
A stabilizer works a site rather than travelling, so its wear tracks operating hours, not distance or the calendar. Scheduling by hours matches service to real use — a machine on a heavy run gets attention before it fails, and a lightly used one isn't serviced needlessly.
What are the signs a spray system needs service?
Uneven or off-spec mix is the giveaway, usually from partly clogged nozzles delivering binder unevenly. Check nozzles for blockage, clean and inspect the spray bars, and flow-test the system rather than assuming it sprays evenly. Many machines let the spray bars slide out for cleaning.
How does HVI help manage stabilizer maintenance?
HVI's preventive maintenance schedules each component by its OEM operating-hour interval, prompts the service before it's due, logs rotor bit wear against hours with a photo record, and routes defects to work orders. It replaces reactive, memory-based upkeep with a schedule that finds you, and keeps an audit-ready history.
Put your stabilizer on a maintenance program that runs itself
HVI schedules rotor, spray, drive and engine PM by operating hours to each OEM's interval, tracks bit wear so replacements are planned, keeps a photo record of every check, and turns a flagged defect into a work order. The machine that quietly leaks fuel and mix quality stops being a mystery. Live in under two weeks.
No credit card · Stabilizer PM schedule ready on day one · Bit tracking built in